Choosing among China’s top storage tubes manufacturers requires more than comparing prices. A reliable supplier should understand the product’s real purpose, storage environment, and handling risks. Tube material matters. Plastic may support impact resistance, while paperboard can offer a lighter and more sustainable option. Diameter, wall thickness, closure design, and internal cleanliness also affect performance.
Michael Chen, a packaging quality consultant with experience in laboratory and industrial containers, says, “A storage tube is not judged by its shape alone; it is judged by what survives inside it.” This practical view should guide every supplier evaluation. Ask manufacturers for production samples, material specifications, dimensional tolerances, and test records. Check whether their equipment can maintain consistent tube length and closure fit. Small differences can create large problems during filling, transport, or long-term storage.
Factory communication deserves equal attention. A professional manufacturer should explain minimum order quantities, lead times, inspection procedures, and corrective actions clearly. Certifications can support trust, but documents alone are not enough. An on-site audit or independent inspection may reveal uneven edges, weak caps, dust, or inconsistent labeling. A low quotation can look attractive. It may also hide limited quality control. I would not choose a supplier from a catalog image alone. The better decision combines samples, technical evidence, production experience, and honest communication. That process takes longer, but it reduces costly surprises.
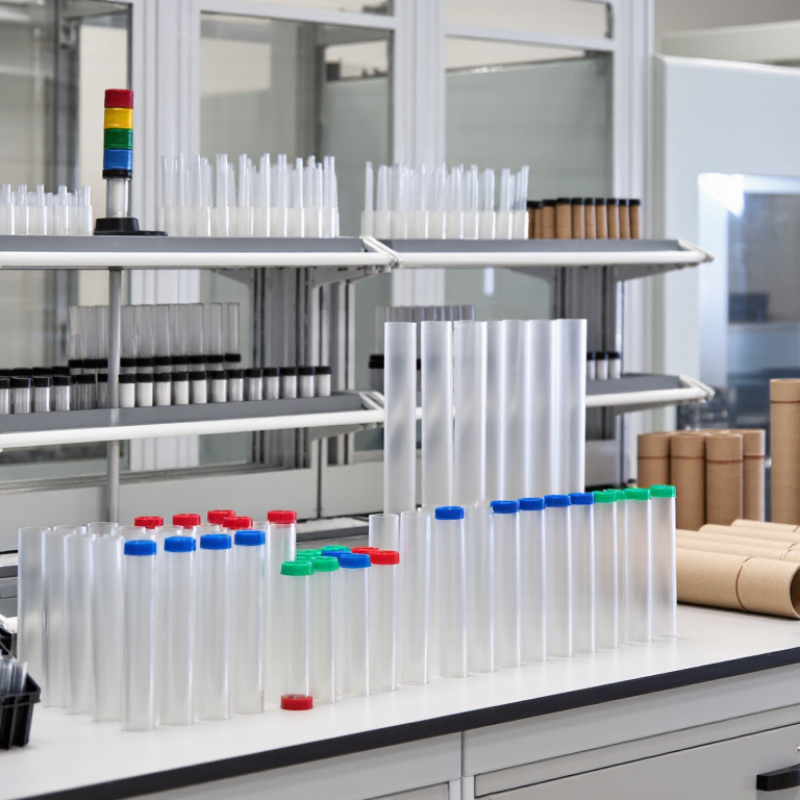
Material density offers a practical starting point when comparing storage tube manufacturers. Polypropylene, or PP, commonly measures 0.90–0.91 g/cm³. Its low weight supports easy handling and economical shipping. PP tubes also provide useful chemical resistance and a firm, slightly flexible feel. High-density polyethylene, or HDPE, usually measures 0.94–0.97 g/cm³. It feels denser and often resists impact better during transport or repeated use. These figures are helpful, but they do not prove quality alone.
During supplier evaluations, request material specifications, batch records, and sample tubes. Check wall thickness near the cap, tube opening, and base. Uneven walls may cause leakage or unstable stacking. A reliable manufacturer should explain resin grades, molding controls, and inspection methods clearly. In practice, I would not choose only by the lowest price. A cheaper tube can create higher replacement costs. Still, density ranges can vary slightly, so buyers should verify actual test results instead of trusting a brochure.
Tips:
Compare PP and HDPE samples under your real storage conditions. Test cap fitting, drop resistance, labeling adhesion, and temperature exposure. Ask whether the material is virgin or recycled. Recycled content may be acceptable, but consistency needs careful checking. One overlooked detail is tube clarity. A clear PP tube may improve visibility, while HDPE can offer stronger opacity and protection from light. The best choice depends on use, not habit.
When choosing a storage tube manufacturer in China, examine its quality system before comparing prices. ISO 9001 shows structured quality management, documented procedures, and controlled corrective actions. However, certification alone is not enough. Request the certificate number, issuing body, scope, and expiration date. Confirm that storage tubes fall within the certified manufacturing activities.
ISO 15378 is especially relevant for primary packaging used in pharmaceutical applications. It combines ISO 9001 principles with GMP requirements for packaging materials. Ask how the factory manages clean production areas, batch records, material identification, and contamination risks. Look for clear traceability from incoming resin to finished tubes. A reliable manufacturer should also explain change control, complaint handling, and CAPA procedures without vague answers. Visit the production site if possible. Observe air filtration, worker gowning, inspection stations, and warehouse labeling.
GMP compliance needs practical evidence. Review recent internal audit records, training files, calibration reports, and sample inspection data. Do not accept polished documents without verification. That shortcut can fail. A small label error may reveal weak controls elsewhere. Ask whether rejected tubes are physically segregated and recorded. Check if quality staff can stop production independently. Some suppliers may have strong certificates but inconsistent daily discipline. That gap deserves attention. The best decision combines valid documentation, factory observations, transparent communication, and repeatable product quality.
| Verification Dimension | Applicable Requirement | Evidence to Request | What to Check During the Audit | Recommended Evaluation |
|---|---|---|---|---|
| ISO 9001 Quality Management System | ISO 9001:2015 provides requirements for a documented quality management system, including process control, risk-based thinking, customer requirements, corrective action, and continual improvement. | Valid certificate, certification scope, certification body details, certificate number, issue date, expiry date, and recent surveillance-audit information. | Confirm that the certificate covers the relevant manufacturing site and storage-tube activities. Review internal audits, management reviews, nonconformance records, CAPA records, and change-control procedures. | Pass only when the certificate is current, independently verifiable, and applicable to the production site. |
| ISO 15378 Primary Packaging Materials | ISO 15378 specifies quality-management-system requirements for manufacturers of primary packaging materials for medicinal products, incorporating GMP principles and risk management. | Valid ISO 15378 certificate, certified scope, site address, product category, audit status, and certification body accreditation information. | Verify control of product-contact materials, contamination risks, traceability, batch documentation, deviations, complaints, and supplier qualification. | High-priority approval criterion when tubes are intended for pharmaceutical or other regulated product packaging. |
| GMP Compliance | Good Manufacturing Practice requires controlled production, hygiene, documentation, qualified personnel, suitable facilities, equipment control, and prevention of contamination and mix-ups. | Applicable GMP certificate or inspection report, site master file where available, hygiene procedures, training records, cleaning records, and environmental-control records. | Inspect personnel flows, material flows, gowning rules, cleaning validation or verification, pest control, foreign-matter controls, and segregation of rejected materials. | Pass when GMP controls are documented, implemented, and supported by objective records. |
| Raw-Material Control | Materials used in storage tubes should be specified, approved, traceable, and suitable for the intended application and product-contact conditions. | Material specifications, certificates of analysis, supplier-approval records, incoming-inspection procedures, and lot-traceability records. | Check resin or laminate identification, storage conditions, status labeling, first-in/first-out controls, and handling of nonconforming materials. | Accept only when every production lot can be linked to approved incoming materials. |
| Process Validation and Control | Critical processes should be defined, qualified where appropriate, monitored, and controlled within approved operating ranges. | Process-flow diagrams, equipment qualification records, validation protocols and reports, control plans, and approved work instructions. | Review controls for forming, trimming, printing, sealing, assembly, cleaning, and packaging. Confirm that process changes require documented approval. | Strong indicator of consistent dimensions, seal integrity, appearance, and functional performance. |
| Cleanroom and Environmental Controls | The required cleanliness level depends on the product risk, intended use, applicable regulations, and customer specification. | Cleanroom classification or monitoring records, temperature and humidity logs, differential-pressure records, cleaning schedules, and maintenance reports. | Confirm monitoring locations, alert and action limits, calibration status, cleaning effectiveness, personnel gowning, and response to excursions. | Risk-based review; do not approve based on a cleanroom label alone. |
| Inspection and Testing Capability | Inspection methods should be suitable for the agreed specifications and should produce reliable, traceable results. | Inspection standards, sampling plans, equipment calibration certificates, test methods, laboratory records, and retain-sample procedures. | Review dimensional checks, weight, wall thickness, leakage or seal testing, visual inspection, compatibility testing, and data-integrity controls. | Pass when results are reproducible, attributable, legible, contemporaneous, original, and accurate. |
| Traceability and Batch Release | Each finished batch should be identifiable from raw materials through production, inspection, release, storage, and shipment. | Batch numbering procedure, batch manufacturing records, release checklist, certificate of analysis, shipping records, and recall or mock-recall results. | Select one completed batch and trace it backward to incoming materials and forward to delivery records. Check authorized release signatures and retention periods. | Mandatory control for regulated or product-contact packaging. |
| CAPA, Complaints, and Change Control | Quality issues should be investigated using documented root-cause analysis, corrective and preventive action, effectiveness checks, and controlled change evaluation. | Anonymized CAPA examples, complaint log, deviation reports, root-cause analyses, effectiveness reviews, and change-control forms. | Check whether investigations address systemic causes and whether customers are notified of changes that may affect form, fit, function, quality, or regulatory status. | Positive sign when records show timely closure and verified effectiveness rather than superficial correction. |
| Supplier and Subcontractor Management | External providers affecting product quality should be evaluated, approved, monitored, and periodically reassessed. | Approved-supplier list, supplier audits, quality agreements, incoming-quality trends, subcontractor controls, and performance reviews. | Determine whether printing, sterilization, testing, assembly, or other outsourced activities are clearly controlled and included in the quality system. | Review carefully because certificates may not cover outsourced operations. |
| Final Supplier-Selection Decision | Certification status should be considered together with product specifications, audit findings, technical capability, regulatory risk, and commercial requirements. | Completed supplier questionnaire, audit report, corrective-action response, approved samples, test results, quality agreement, and documented risk assessment. | Confirm that all critical findings are closed or formally accepted before mass production. Establish ongoing monitoring and periodic requalification. | Approve conditionally or fully according to documented evidence and application risk. |
Note: ISO certification and GMP evidence should be verified with the issuing certification body or relevant regulatory authority. Acceptance criteria should be adjusted to the intended market, product-contact risk, and applicable customer requirements.
Choosing among China’s top storage tube manufacturers requires more than comparing catalog sizes. Capacity should be measured as usable volume, not only nominal capacity. A 10 mL tube may hold less after the cap and shoulder geometry are considered. Request dimensional drawings and verify samples with calibrated water or gravimetric testing. Record the average volume and the variation between ten tubes.
Wall thickness reveals manufacturing consistency. Measure several points around the body, base, and threaded neck with a thickness gauge. Uneven walls can cause deformation during transport or temperature changes. A thicker tube is not automatically better. Excess material may reduce flexibility and increase cost. Look for stable readings across batches, supported by inspection records and material specifications.
Leak-rate data deserves careful attention. Ask whether testing used pressure, vacuum, dye, or helium methods, and record the test duration. A leak rate without pressure, temperature, and acceptance limits is incomplete evidence. Practical testing can include filled tubes stored upright, inverted, and horizontally before inspection. Check the closure after repeated opening cycles. Small errors matter.
I once selected a tube using capacity alone. The fit looked correct, but the seal weakened after cold storage. That changed my selection process. Compare performance data under your actual temperature, filling, and handling conditions. Ask for recent batch reports, sample retention rules, and corrective-action records. Reliable manufacturers explain failed tests instead of hiding them. Some data may still be imperfect, so independent verification remains worthwhile.
Choosing a storage tube manufacturer requires more than comparing unit prices. In production reviews, customization often reveals a supplier’s real capability. Ask whether the factory can adjust diameter, wall thickness, cap fit, color, printing, and material grade. Request a drawing with tolerances, not only digital pictures. A physical sample should confirm grip, closure strength, surface finish, and label placement. Small errors matter. A cap that loosens during transport can damage the entire shipment.
MOQ deserves careful calculation. A low MOQ may help market testing, but it can increase tooling or per-unit costs. A high MOQ can reduce pricing while creating inventory pressure. Ask for separate quotes for samples, pilot orders, and repeat production. Clarify whether existing molds are available and who owns new tooling. Tooling charges should include mold life, maintenance, revisions, and storage terms. These details are often overlooked. No forecast is perfect.
A typical production window is 15–30 days after artwork, specifications, and payment are approved. Confirm what the lead time includes. It may exclude sampling, mold making, holiday shutdowns, inspections, or shipping. Reliable suppliers provide a schedule with approval points and inspection records. Check material certificates, batch consistency, and packaging tests before mass production. Build a small buffer. Delays still happen, even with careful planning. A written change-control process protects both sides when requirements shift.
Typical planning ranges for customization, minimum order quantity, tooling costs, and production lead times.
Stock sizes usually offer the shortest schedule. Custom colors, printing, closures, and structures require additional approval and production time.
Common planning ranges are about 500–2,000 pieces for customized orders and 2,000–5,000 pieces for new structures or special finishes.
Simple custom molds often require approximately US$1,500–8,000, depending on material, cavity count, dimensions, and surface details.
The figures are general industry planning benchmarks. Actual MOQ, tooling quotations, and delivery dates depend on product specifications, sampling approval, order volume, and production capacity.
China Top Storage Tubes Manufacturers: How to Choose?
Export capability should be tested, not assumed. The World Bank’s Logistics Performance Index 2023 gave China a score of 3.7 out of 5 and ranked it 19th globally. This indicates strong logistics, but it does not prove one factory ships reliably. Ask for recent bills of lading, export destinations, carton photos, and on-time delivery records. Compare these details with declared production capacity.
Testing reports should identify the exact tube material, batch number, test date, and laboratory accreditation. For plastic storage tubes, review wall thickness, drop resistance, closure torque, leakage, and chemical compatibility. Food-contact applications need applicable regional compliance evidence, not a generic “food grade” statement. Also check REACH or RoHS documentation when markets require it. ISO 9001 certification can support process control, but its scope and validity must be verified. A certificate without factory records is weak evidence.
Factory data makes the audit more practical. Request molding-machine lists, daily output, defect rates, inspection plans, and retained samples. The International Trade Centre reports China remained the world’s largest merchandise exporter in 2023, with exports exceeding 3.3 trillion US dollars. Scale helps, yet scale can hide uneven quality between production lines. One uncomfortable point: many audits rely too heavily on polished documents. Visit the line, inspect resin storage, and watch closure testing. A missing batch label or inconsistent wall thickness deserves a written corrective action.